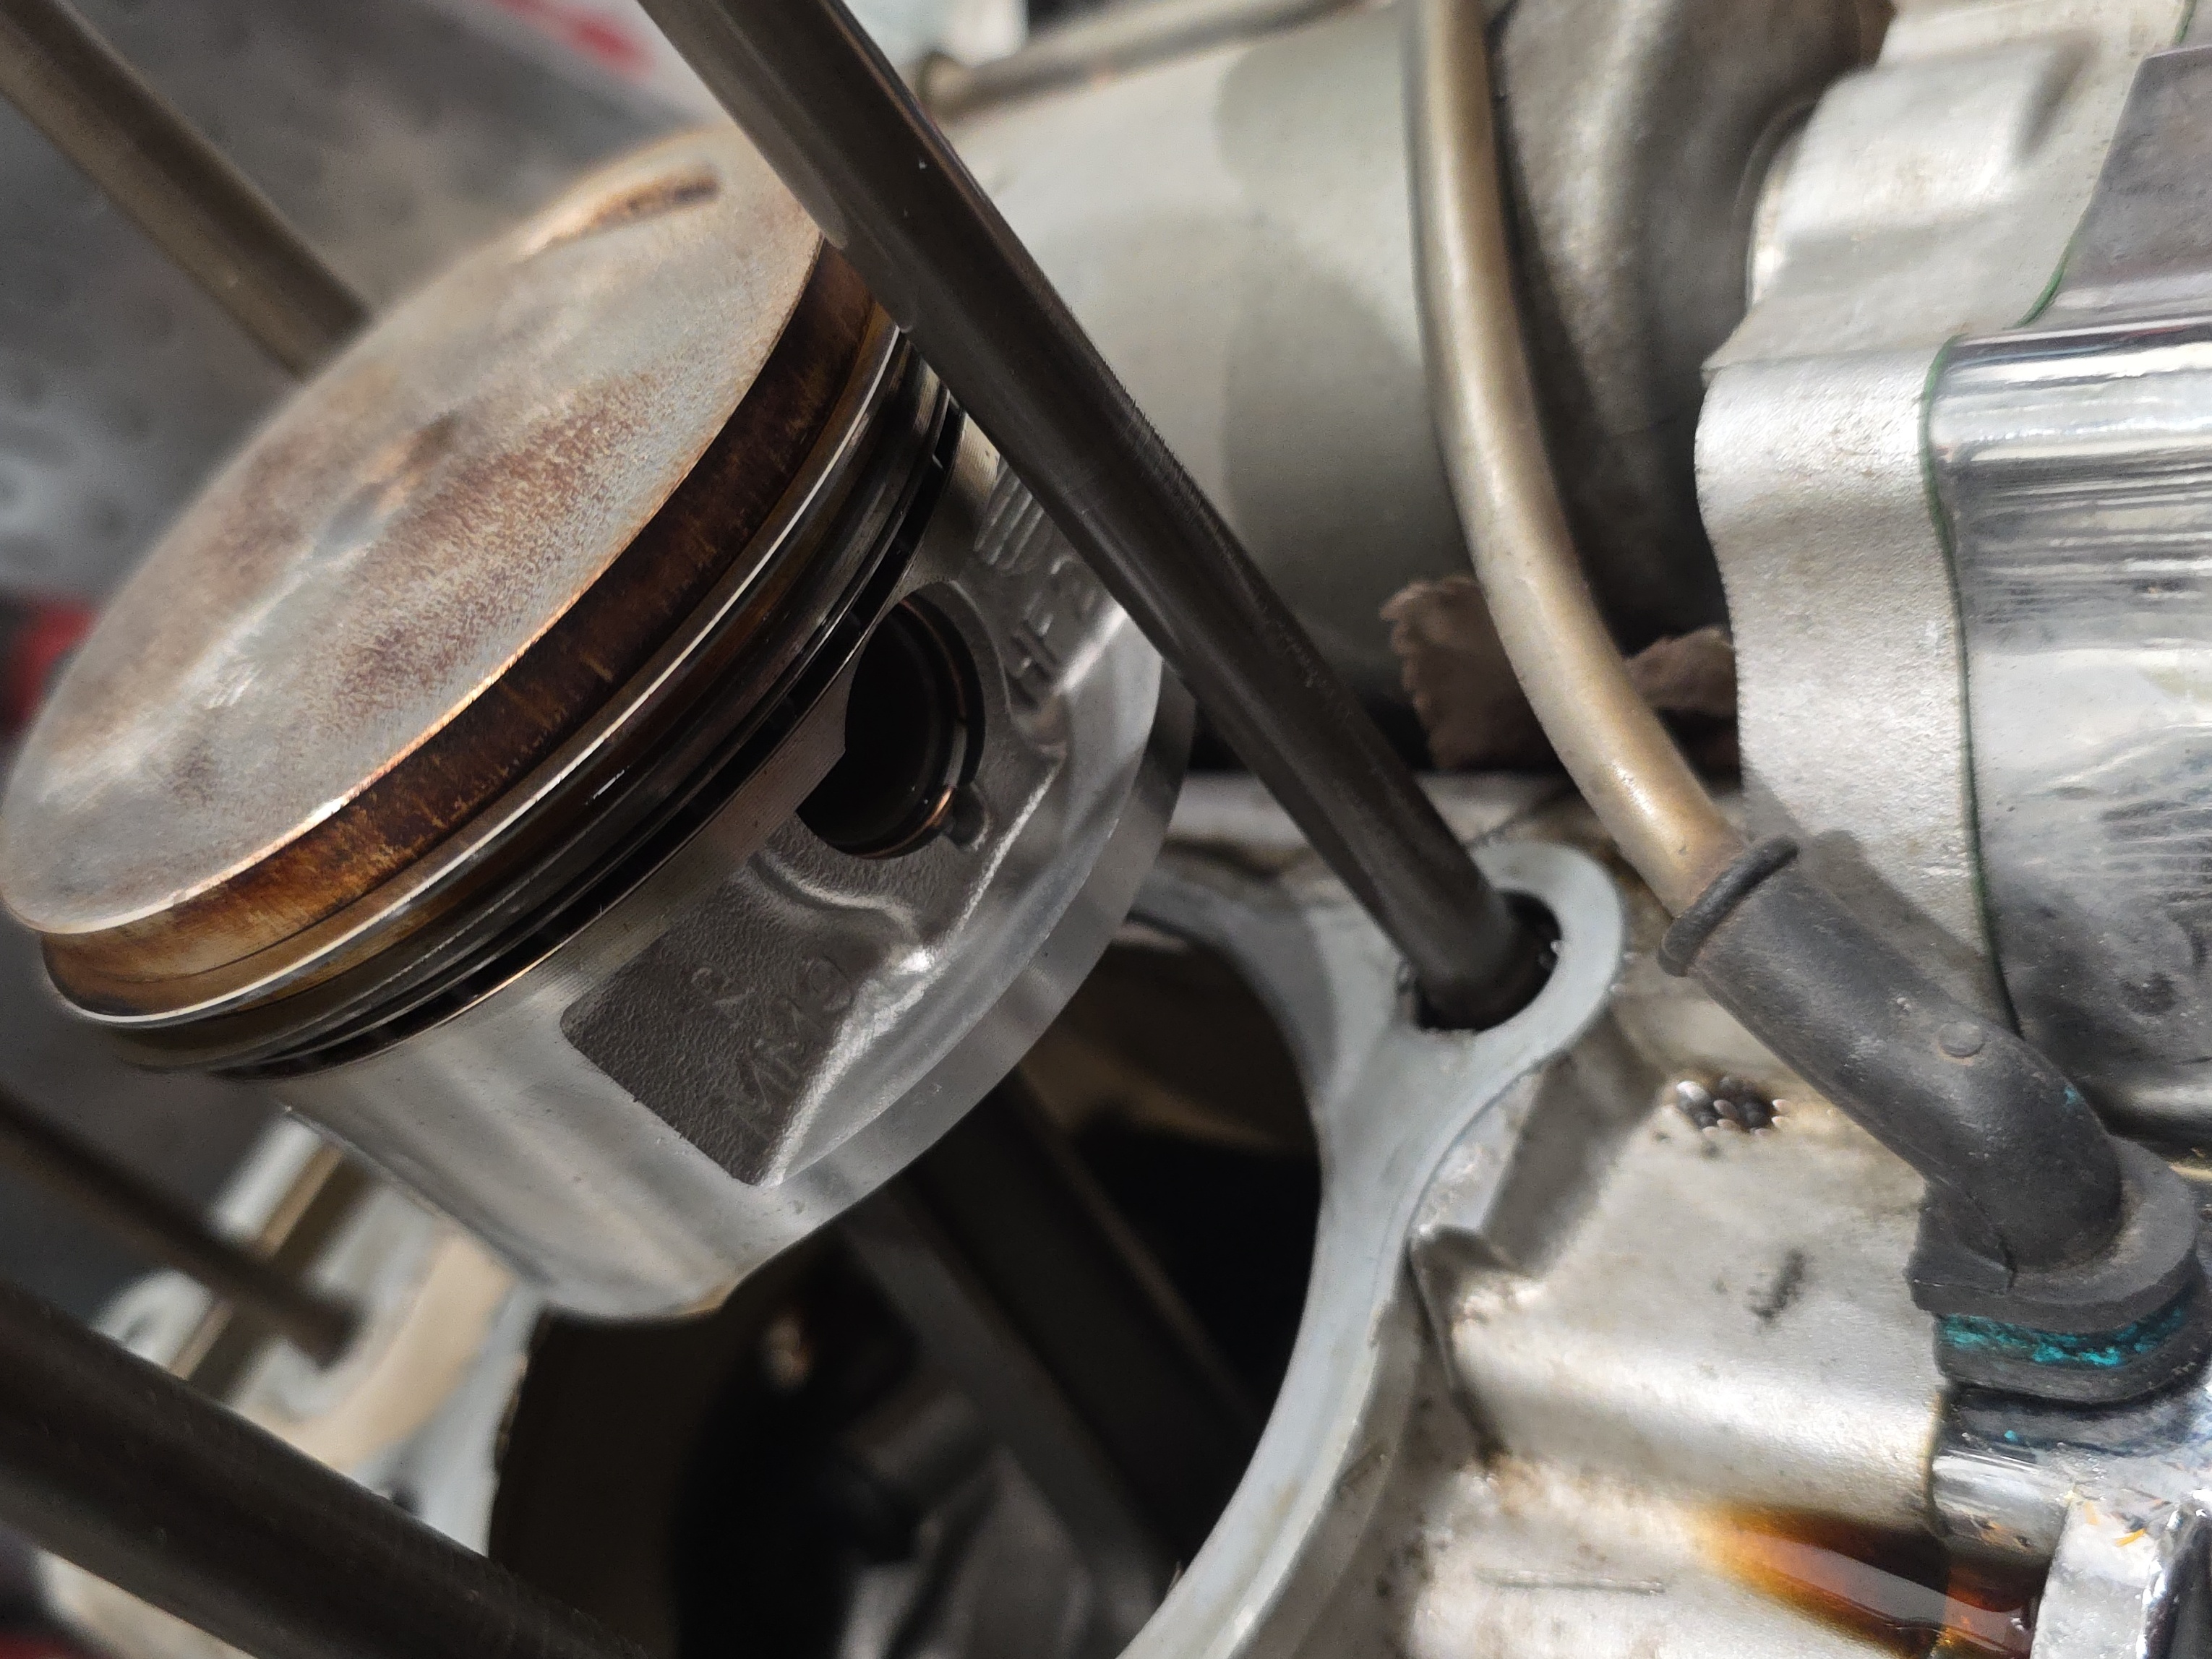
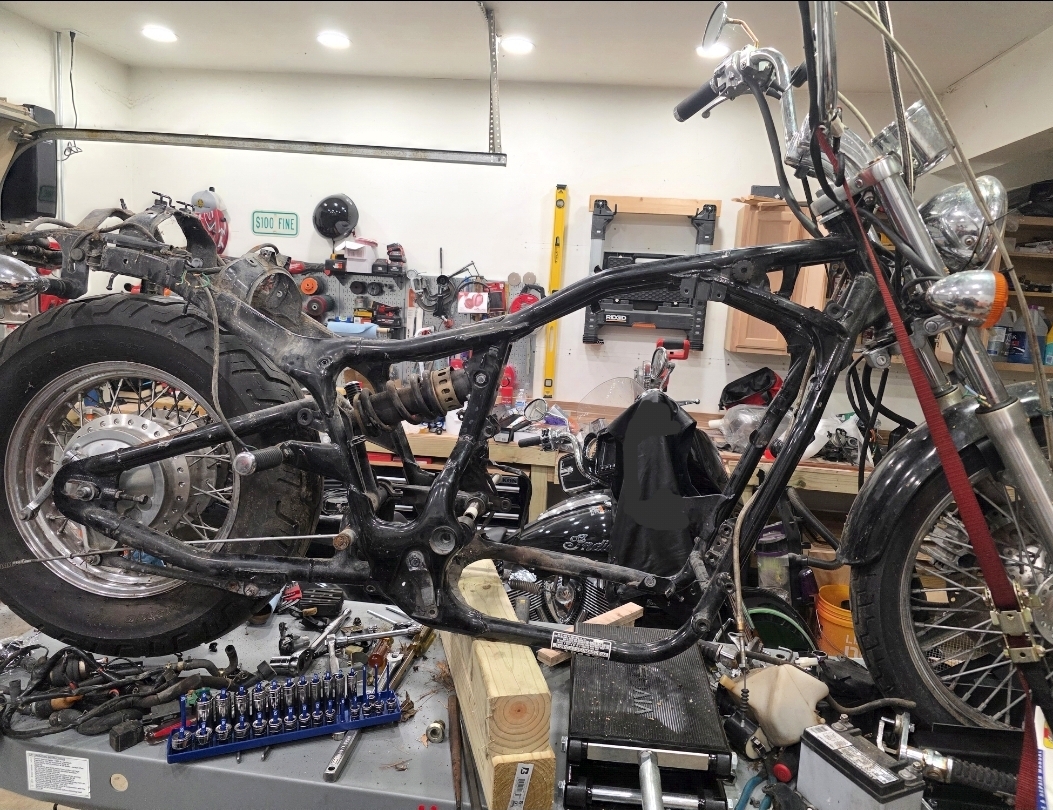
Im overhauling my 97 shadow 600. Boot burner exhaust, velocity stacks, re jetting the carbs, new penut gas tank, e tank and small battery box, going to re wire the bike and run the wires through the frame, hard tail weld on kit, springer seat, springer forks, replacing starter motor, clutch plates, lapped the valves, re honed the bores.
Idk what happened to the rest of my post
So the current issue im having is finding new piston rings. I tried buying some off ebay but they are using some crap shipper and I dont think they are coming. Im ready to start cutting the frame for the hard tail kit but I need to get this engine buttoned up to keep the grinding dust out of it...
@Michael r well how much bigger did you hone? You can still get the 0.25 pistons from partzilla i know that. t.ly/yBg-6
@TJ not much just took the glaze off and re crosshatchted. Awesome! Partzilla keeps saying it dosent fit my vehicle so I was hesitant on purchasing it. Thank you!
One other question. For the hard tail mod. I need to weld in the crossbar. I am also waiting on the springer seat to arrive. Do you know how far down I should weld it from that lower gas tank bolt hole? Thank you for you're help you have really made my first time bike rebuild easy and enjoyable.
@Michael r make sure you can return the part if for some god forsaken reason it doesnt fit.
for the wishbone crossmember, mount your solo seat with springs, where the springs land between the wishbone, thats where you put the crossmember. also, have your rear wheel installed with a new tire. push the axle to the forward most running position in the axle plates and tighten it down. put a length of chain on the crown of the tire, tape it down, and set your fender on there, so it extends past the point where the crossmember would land.
this will also help ensure you dont put the crossmember so far back that it interferes with the tire, or prevents you from mounting a fender properly.
make good fishmouths on the tube, chamfer, and clean all surfaces. tac in place, check for square and test and test again before final weld.
 TJ Admin Staff memberModeratorMember who has the rights to delete posts, and ban members form forum if they violate the rules.